SIGER Thermal Compensation Management System V1.1 Version Released
SIGER Thermal Compensation Management System V1.1 Version Released.
The SIGER Thermal Compensation Management System reduces thermal errors caused by temperature changes during the machining process of CNC machines through measurement and compensation systems, thereby improving machining accuracy and stability; Based on the embedded structure of machine tools and combined with a thermal error compensation model, real-time compensation values are output to effectively improve product processing accuracy and reduce product scrap rates.
SIGER Thermal Compensation Management System
The core functions of the machine tool Thermal Compensation Management System are as follows:
■ Real time monitoring of spindle temperature information based on temperature acquisition at the X-axis, Z-axis guide rails, and bearing seats.
■ Construct a temperature difference compensation model through polynomial regression analysis of temperature rise and thermal error at the guide rail and bearing seat.
■ Based on the temperature changes from the cold machine to the hot machine, combined with the analysis results of the algorithm, calculate the error compensation value, call the data acquisition service, and use the macro variable assignment method to send the error compensation value to the machine tool.
SIGER Thermal Compensation Management SystemApplicable machine tool types
Machining centers, turning and milling composites, lathes, etc.
Applicable control systemApplicable processing technology
Multiple processes including large-scale repetitive processing, large-scale nested processing, long-term mold processing, small-scale processing, rough/fine processing, etc.
Applicable processing scenarios
Long term processing scenarios such as mold processing, equipment manufacturing, large automotive parts, and aerospace.
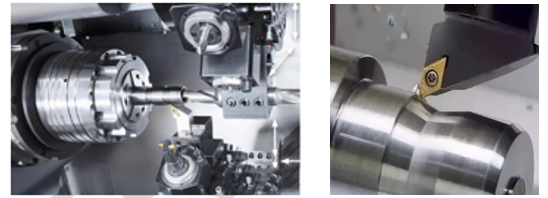
SIGER Thermal Compensation Management System
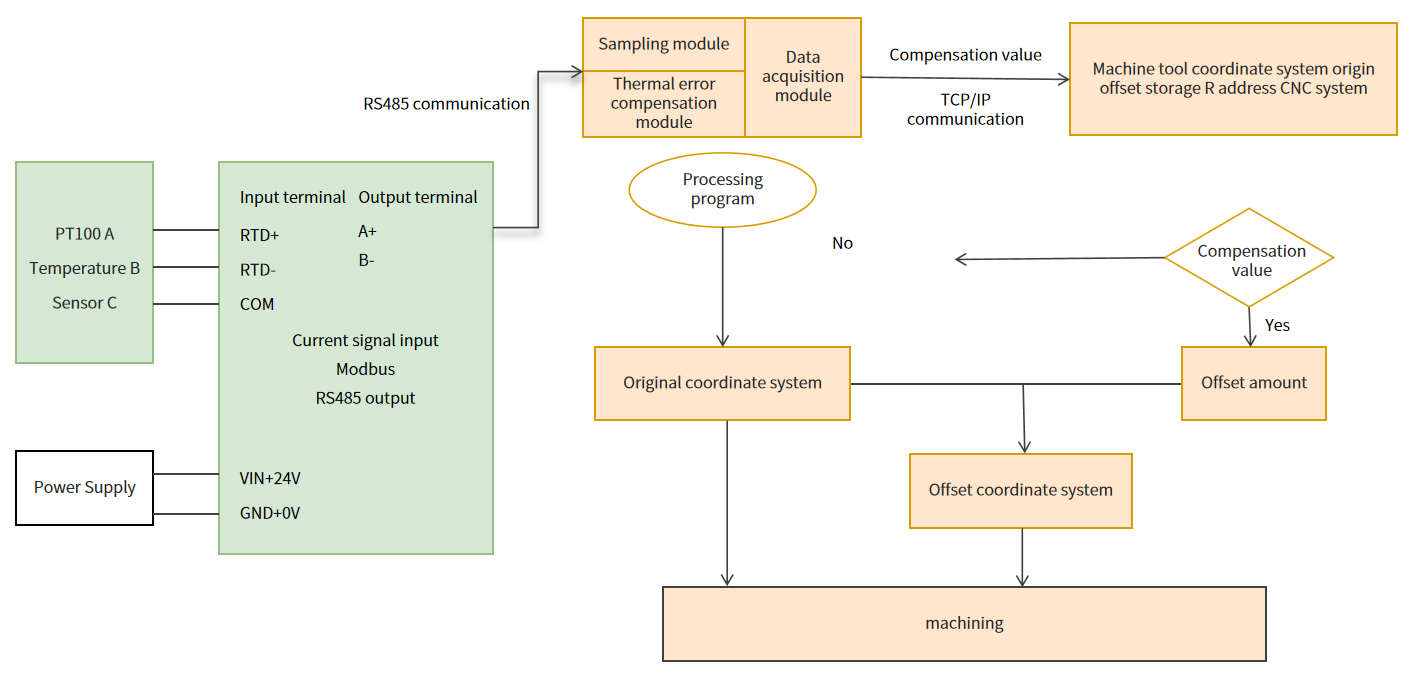
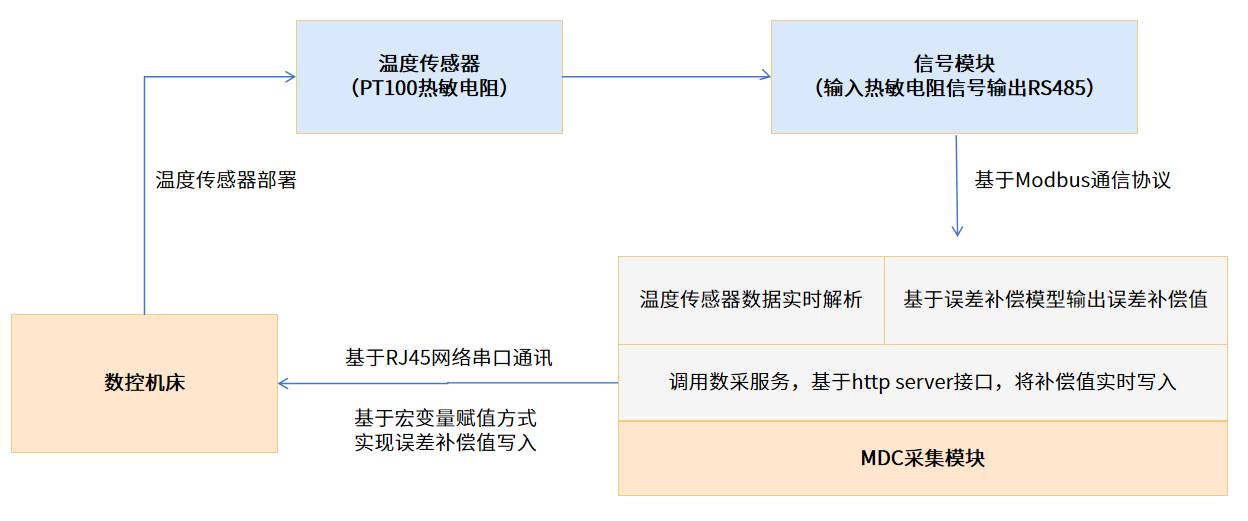
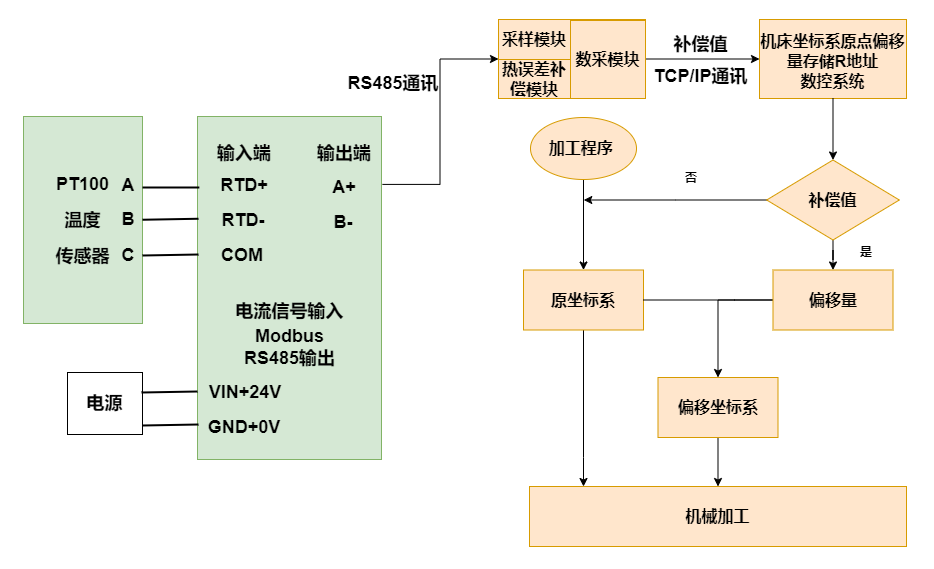
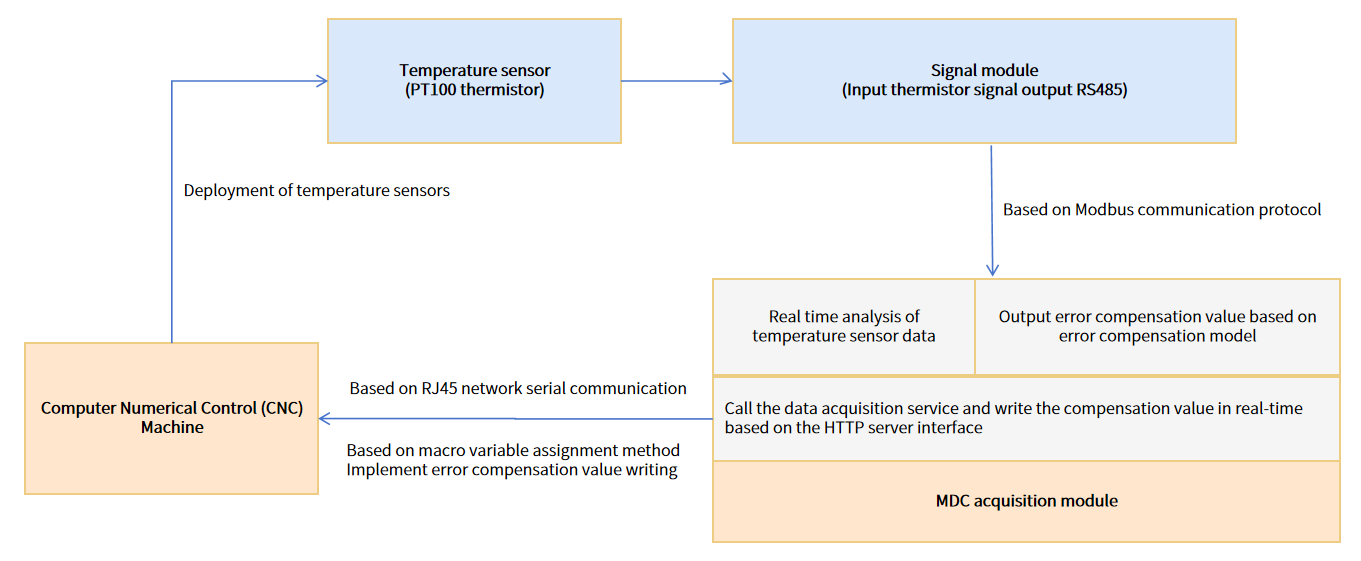
Figure: Principle of Error Compensation
▶ Real time writing of machine tool R address data is achieved through communication between data acquisition services and machine tools.
▶ Real time parsing of temperature sensor data using Modbus communication protocol.
▶ Establish the binding relationship between temperature sensors and various axes (X, Y, Z, and spindle) of the machine tool.
▶ Clean and process the collected temperature data to remove outliers and ensure data quality.
▶ Calculate the error variation Δμ based on real-time temperature data.
▶ According to the preset compensation model and the relationship between each axis of the machine tool, when the error change exceeds the set threshold, the corresponding compensation value is output through linear interpolation and other methods.
▶ Use the HTTP Server interface to write the compensation value in real-time to the corresponding R address of the machine tool.
▶ Real time temperature data is stored offline, including key information such as timestamp, reporting frequency, axis number (such as X, Y, Z, and spindle), etc.
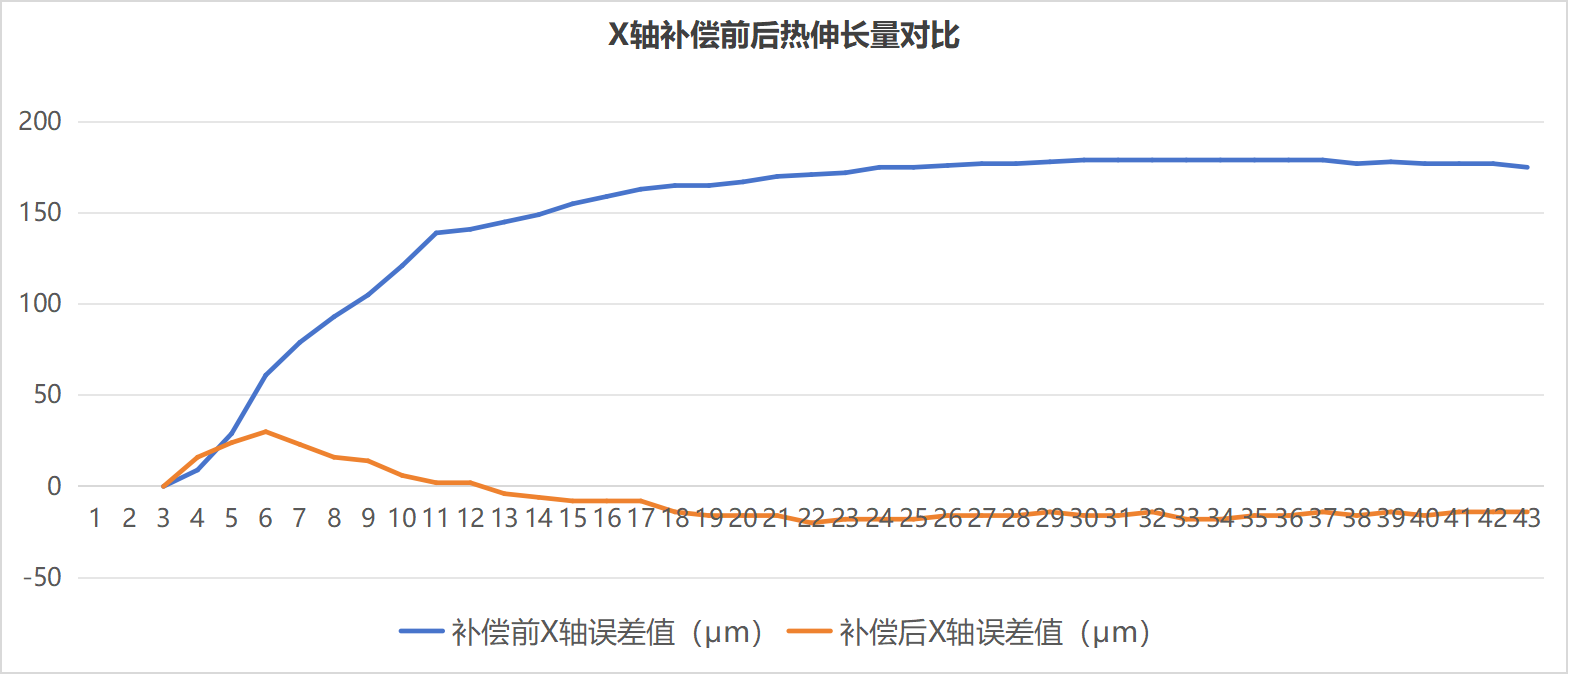
SIGER Thermal Compensation Management SystemComparison results of X-axis thermal elongation and temperature change tests
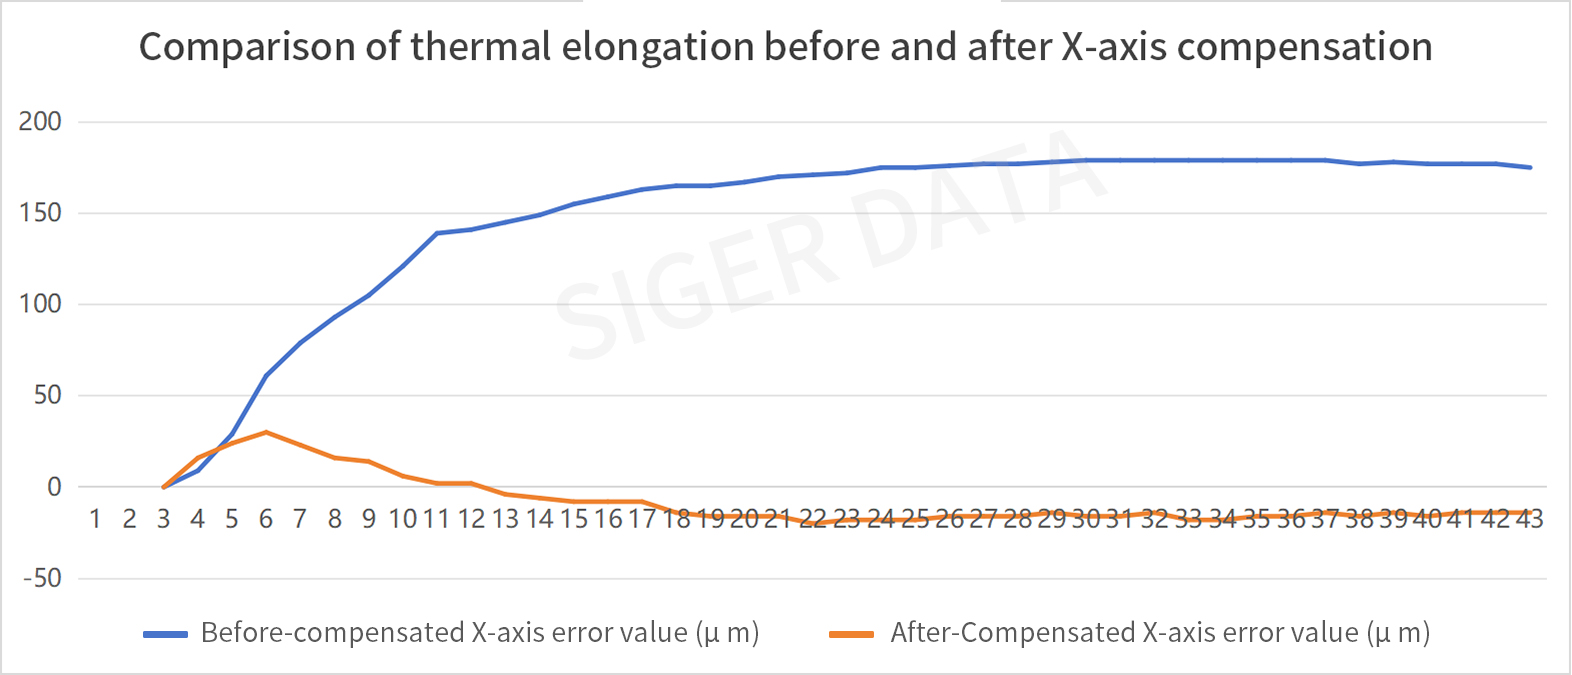
Unopened thermal compensation:
X-axis thermal elongation changes by 175 μ m, spindle motor temperature changes by 11.7 ℃.
Enable thermal compensation:
X-axis thermal elongation changes by 50 μ m, spindle motor temperature changes by 10.9 ℃.
Application effect:
The thermal elongation has been reduced by 125 μ m, and the thermal compensation effect can reach 71.42%.
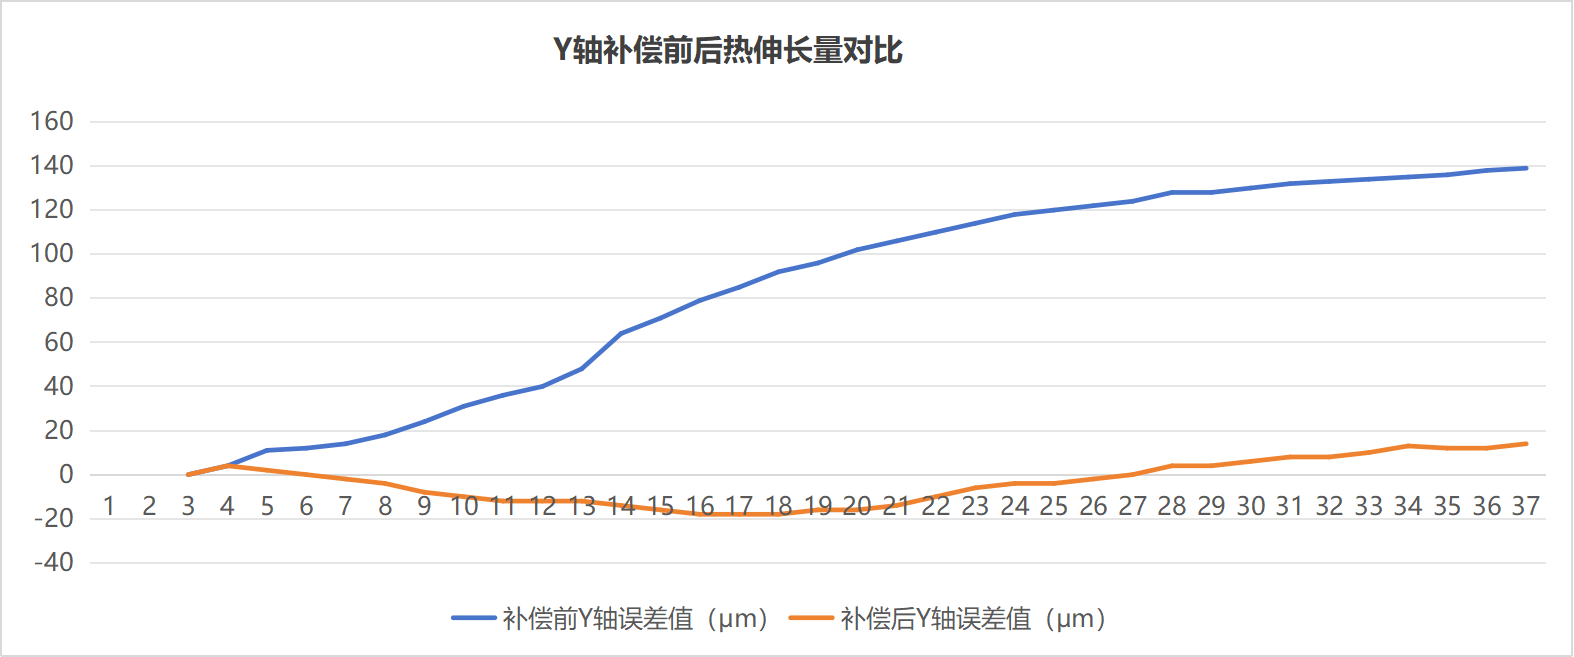
Comparison results of Y-axis thermal elongation and temperature change tests
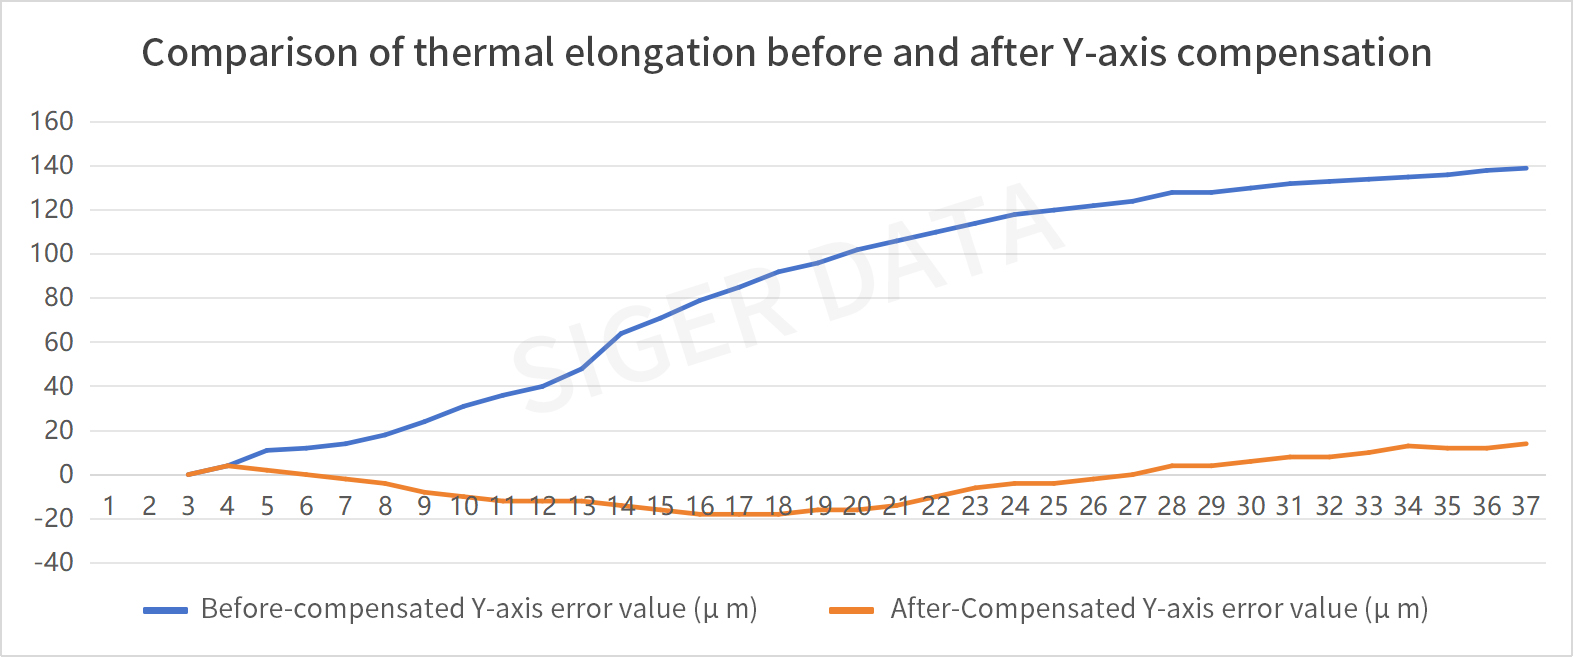
Unopened thermal compensation:
Y-axis thermal elongation changes by 144 μ m, spindle motor temperature changes by 6.1 ℃.
Enable thermal compensation:
Y-axis thermal elongation changes by 32 μ m, spindle motor temperature changes by 5.2 ℃
Application effect:
The thermal elongation has been reduced by 112 μ m, and the thermal compensation effect can reach 77.78%.
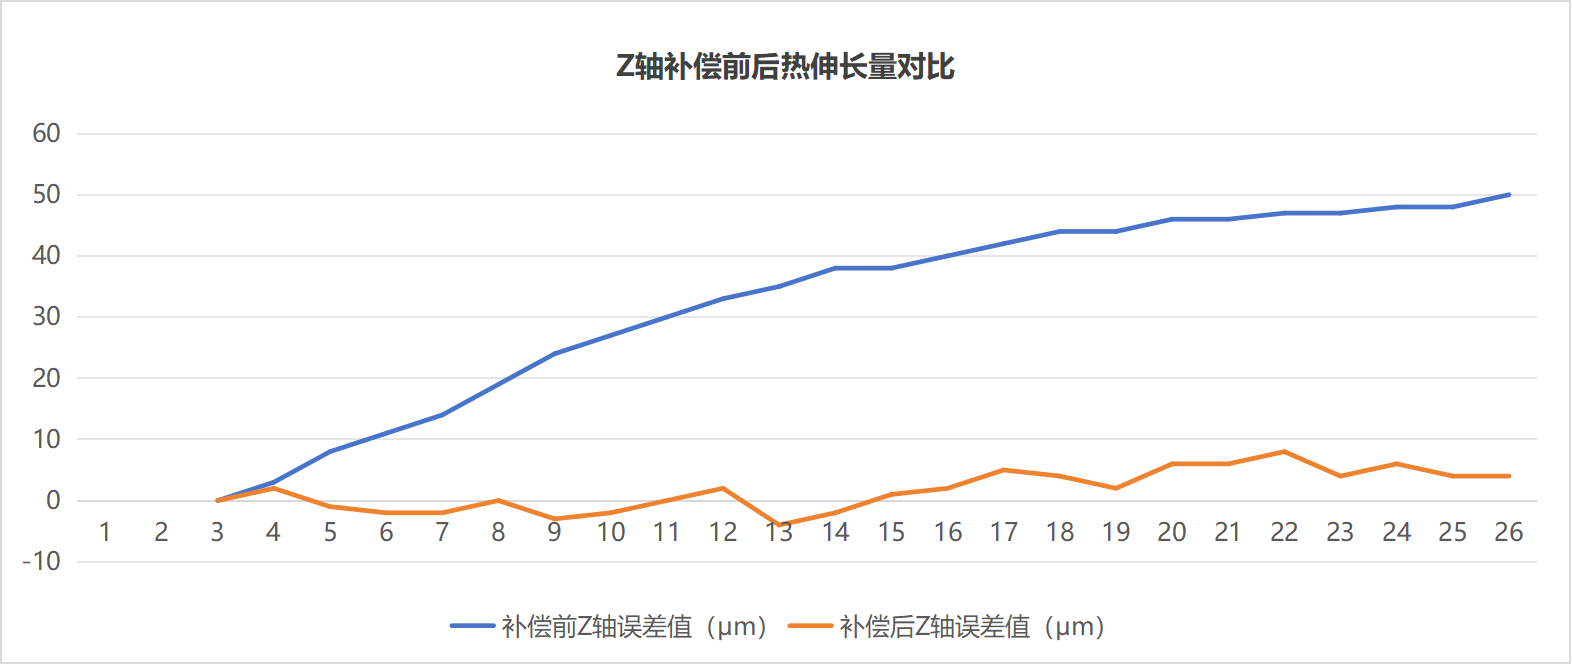
Comparison results of Z-axis thermal elongation and temperature change tests
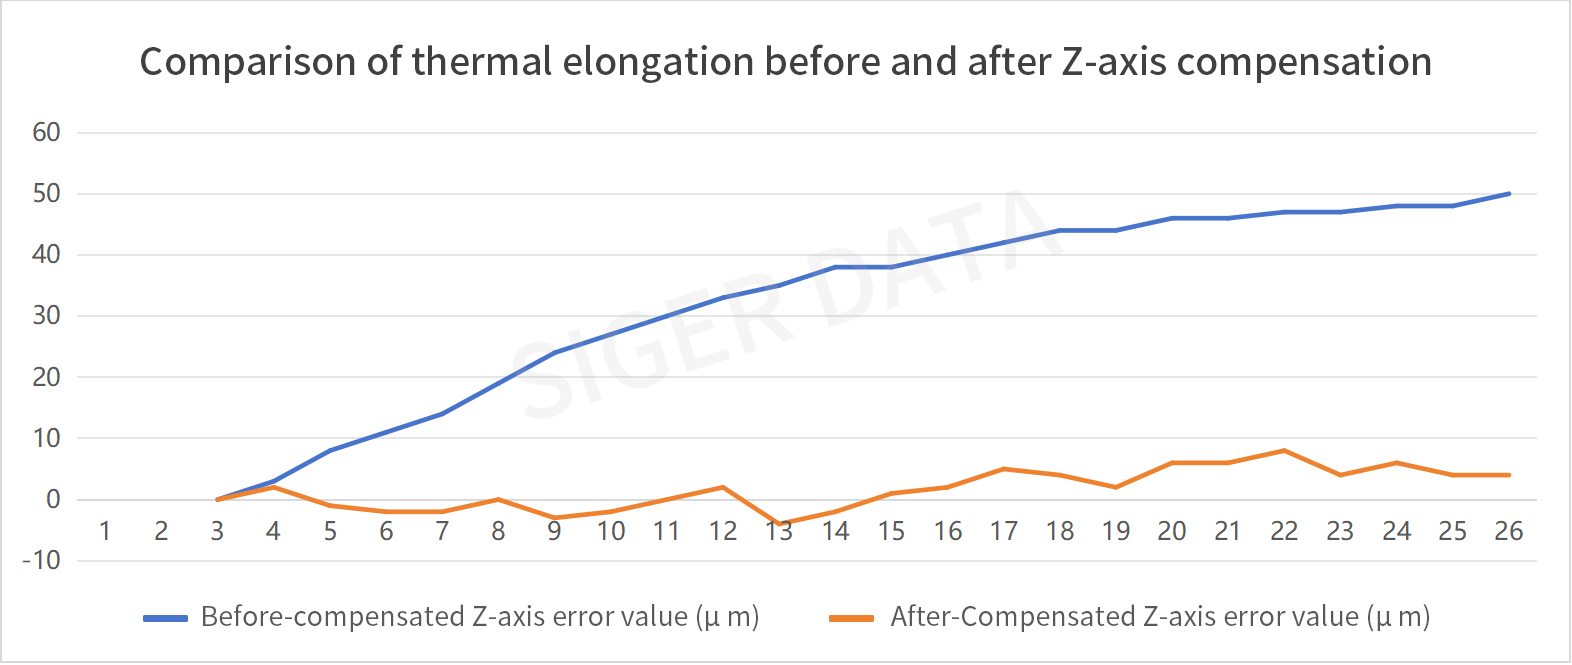
Unopened thermal compensation:
Z-axis thermal elongation changes by 53 μ m, spindle motor temperature changes by 3.5 ℃.
Enable thermal compensation:
Z-axis thermal elongation changes by 12 μ m, spindle motor temperature changes by 2.2 ℃
Application effect:
The thermal elongation has been reduced by 41 μ m, and the thermal compensation effect can reach 77.36%.
The functions introduced above belong to the Thermal Compensation Management System independently developed by SIGER. This release is version 1.1, and more functions will continue to be iterated and updated. Stay tuned!
If you are interested in SIGER products, you can contact us by phone or email, or submit your requirements by leaving a message, and we will arrange personnel to contact you as soon as possible.
--------------------------------------------------------------------------------------------------------------------------------------------------------
Official Contact Info:
Email: marketing@siger-data.com
WhatsApp:+86 189 6235 3927
WeChat:189 6235 3927