SIGER i-NC Mold Precision Optimization System V1.1 has been officially released
Jiangsu SIGER Data Technology Co., Ltd. (referred to as SIGER) and Wuhan Hanmai Technology Co., Ltd. (referred to as Hanmai Technology) officially announced the release of i-NC product V1.1 version on November 27, 2023.
SIGER i-NC
This product is developed by Professor Li Zhenhan leading a team of PhD and master's degree holders, who have completed comprehensive development work such as real-time measurement, geometric calculation, and tool motion control optimization, enabling i-NC to possess motion control and computational geometry technology optimization capabilities. This product will further enhance SIGER's product service capabilities in the field of precision machining for tool path calculation and control, forming a closed loop for tool monitoring applications and geometric trajectory optimization, laying a foundation for providing higher precision products and services for the precision machining industry.
SIGER i-NC Mold Precision Optimization System
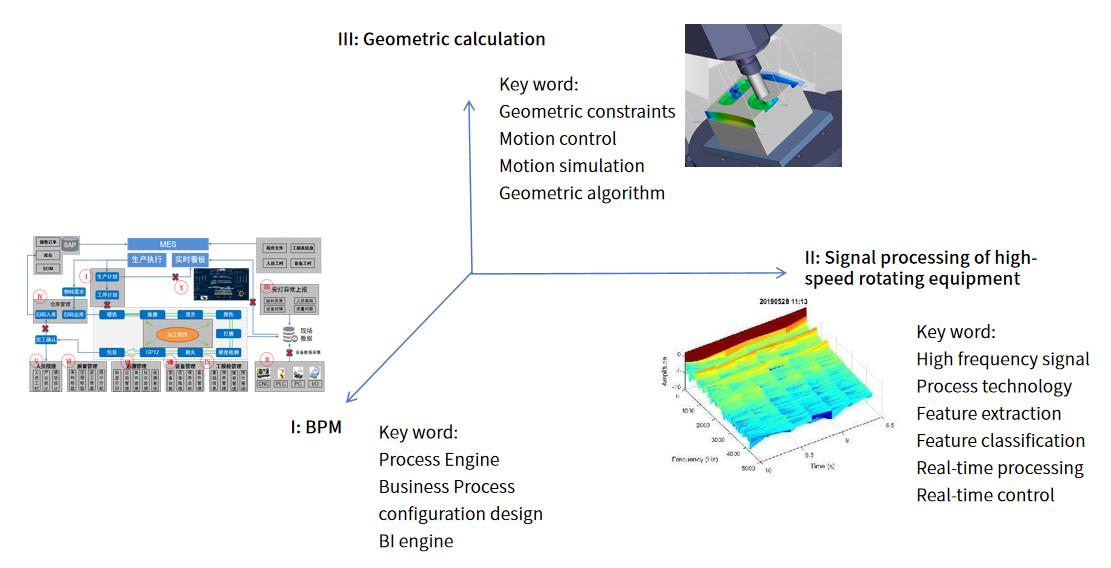
Three dimensional diagram of precision machining process management
During the processing of traditional large molds, problems such as thermal deformation of the lead screw caused by gantry motion, lack of smooth compensation for tool wear, cumulative errors in AB mold clamping, and spatial deformation caused by the gravity of the large mold itself can be addressed. SIGER and Hanmai Technology provide a one-stop real-time online optimization system to ensure product accuracy.
Business Structure Diagram
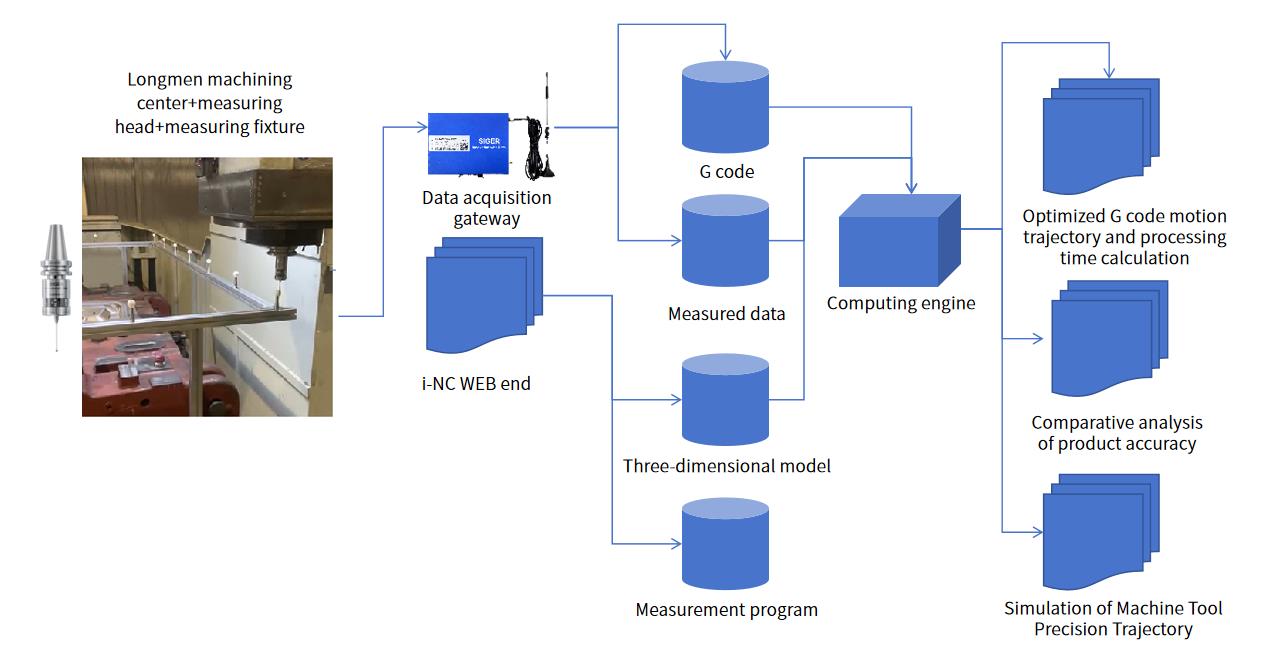
The product design covers real-time acquisition of machine tool data, real-time acquisition of 3D data, and acquisition of machine tool and tool parameters. Combined with real-time measurement, corresponding process variation calculation and trajectory optimization are completed to achieve tool trajectory optimization and accuracy control.

The effective decomposition and real-time optimization steps of the i-NC system implementation process are as follows:
Step 1. Install standard balls according to the established design
Step 2. Measure the 4 points on each standard sphere and the highest point on the sphere using the "4-point center" method, and record the original data
Step 3. Change the measurement height and repeat the above measurement twice
Step 4. Based on the comprehensive analysis of the three sets of results, the conclusion is drawn that:
For the attitude error of the measuring head, it can be corrected by modeling and calculating the error compensation amount.
If the posture of the measuring head is not parallel to the Z-axis of the machine tool, measurement errors will occur as shown in the following figure:

Axis repeatability accuracy variation chart:

The overall product is as follows:

Based on the measurement results of blue light 3D scanning, the trajectory accuracy deviation without optimization is as follows:

The effect of optimizing the tool path temperature difference deformation compensation based on i-NC measurement is as follows:

■ Region 1 represents the machining area of E13218D (optimized trajectory) (near the tool mark)
■ Region 2 represents the processing area of E13218B (near the knife mark)
■ Region 3 represents the processing area of E13218C (near the knife mark)
■ Region 4 represents the processing area of E13218A (near the knife mark)
Region 1:

Region 2:

Region 3:

Region 4:

The comprehensive accuracy of i-NC has been improved by 58.65%, greatly improving the precision of mold processing, and will continue to be applied in various aspects of precision machining to help customers achieve high-precision machining; The subsequent product design and optimization will continue to focus on the thermal deformation of the lead screw caused by the gantry movement process, the lack of smooth compensation for tool wear, the accumulation of errors in AB mold clamping, and the spatial deformation caused by the gravity effect of large molds themselves, in order to provide users with better products and services.
The functions introduced above belong to the i-NC product V1.1 version officially released by SIGER and Hanmai Technology on November 27, 2023. More functions will be gradually iterated and updated. Stay tuned!
If you are interested in SIGER products, you can contact us by phone or email, or submit your requirements by leaving a message, and we will arrange personnel to contact you as soon as possible.
--------------------------------------------------------------------------------------------------------------------------------------------------------
Official Contact Info:
Email: marketing@siger-data.com
WhatsApp:+86 189 6235 3927
WeChat:189 6235 3927